2016年5月29日星期日

Cold die clearances between control and adjusting  method
  Cold stamping mould convex, concave die size and distribution of the clearance degree directly affect the quality of the blanking pieces and the length of the service life of the die. Precision stamping partsIn guarantee blanking pieces space is mould manufacturing assembly very important link, and assembly quality will directly influence the convex, concave die if the clearance between the uniform. Such as the process of convex, concave die size precision although already meet the requirements, but in assembling if adjustment is bad, can cause clearance does not even, rushed out of the spare parts of the raw edges. Even rushed out of unqualified parts. The mold assembly is key to control convex, concave die of relative positions, in order to ensure that the convex, concave die, uniform and the clearance between the right to rush out of qualified parts.
 Die before assembly the problems that should be paid attention
   Convex, concave die and mould parts itself is clearance of the precision, and the assembly of the assembly process is reasonable. In order to ensure that the position of the convex, concave die correctly and gaps even, mould design, processing to assembly from the whole link should pay attention to the following questions:
   (1)Convex, concave die design and manufacture of the right
  Design should be based on the above all when die cutting the section of a quality, service life of die factors such as the reasonable selection of convex, concave die clearance. And to consider the mould in the process of using that gap wear increases, Precision stamping parts general in the design the least reasonable clearance when mould. And in the manufacturing process can ensure the parts processing precision and quality, in the assembly process ensure convex, concave die gap even, this for processing complex shape is very key parts.
 (2)Assembly method the choice should be reasonable 

   Die assembly method include roughly assembly method and direct with assembly method. Before the assembly must be carefully study mold assembly drawing, full consideration and analysis of the structure characteristics of punching die, Precision stamping partsdie parts processing technology and processing accuracy etc, in order to choose convenient, accurate and reliable assembly method to ensure the quality of blanking pieces
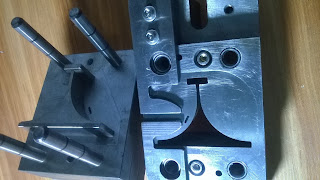
  Precision stamping parts

2016年5月25日星期三

Renoho Precision Machinery Technology Co.,Ltd: Cold die clearances between control and adjusting ...

Renoho Precision Machinery Technology Co.,Ltd: Cold die clearances between control and adjusting ...: Cold die clearances between control and adjusting method  Cold stamping mould convex, concave die size and distribution of the clearance ...

Cold die clearances between control and adjusting method

Cold die clearances between control and adjusting method
 Cold stamping mould convex, concave die size and distribution of the clearance degree directly affect the quality of the blanking pieces and the length of the service life of the die. Precision stamping parts In guarantee blanking pieces space is mould manufacturing assembly very important link, and assembly quality will directly influence the convex, concave die if the clearance between the uniform. Such as the process of convex, concave die size precision although already meet the requirements, but in assembling if adjustment is bad, can cause clearance does not even, rushed out of the spare parts of the raw edges. Even rushed out of unqualified parts. The mold assembly is key to control convex, concave die of relative positions, in order to ensure that the convex, concave die, uniform and the clearance between the right to rush out of qualified parts.
 Die before assembly the problems that should be paid attention 
 Convex, concave die and mould parts itself is clearance of the precision, and the assembly of the assembly process is reasonable. In order to ensure that Precision stamping parts the position of the convex, concave die correctly and gaps even, mould design, processing to assembly from the whole link should pay attention to the following questions: 
 (1)Convex, concave die design and manufacture of the right
Precision stamping parts Design should be based on the above all when die cutting the section of a quality, service life of die factors such as the reasonable selection of convex, concave die clearance. And to consider the mould in the process of using that gap wear increases, general in the design the least reasonable clearance when mould. And in the manufacturing process can ensure the parts processing precision and quality, in the assembly process ensure convex, concave die gap even, this for processing complex shape is very key parts.
  (2)Assembly method the choice should be reasonable   

 Die assembly method include roughly assembly method and direct with assembly method. Before the assembly must be carefully study mold assembly drawing, full consideration and analysis of the structure characteristics of punching die, die parts processing technology and processing accuracy etc, in order to choose convenient, accurate and reliable assembly method to ensure the quality of blanking pieces.

 Precision stamping parts

2016年5月23日星期一

The surface of the mold heat treatment to strengthen the quality and impact on life

The surface of the mold heat treatment to strengthen the quality and impact on life  
 Mold heat treatment the nature and quality of life of the mold a great impact. Practice shows that the die parts of the quenching distortion and cracking, early fracture during use, while the metallurgical and materials quality, forging quality, cnc machining parts mold structure and process related, but related more to die of heat treatment. According to statistical analysis of failure causes of mold, heat treatment failure due to improper accounting for more than 50%. Practice shows that the mold material must be accompanied by high heat treatment process properly, can really play a material's potential. Parts surface hardening mold work purpose is to obtain the effect of external hard tough inside, so be hardness, wear resistance, toughness, good resistance to fatigue with. Many ways to die surface hardening, surface treatment technology of new technologies developed rapidly. In addition to Nitrocarburizing and ion nitride, boride, seepage niobium, vanadium permeability, hard chrome plated and spark strengthening, the chemical vapor deposition (CVD) and physical vapor deposition (PVD) has been gradually adopted. By CVD and PVD treatment, the mold surface covered with super-hard material, such as TiC, TiN, etc.. High hardness, wear resistance, corrosion resistance, adhesion is very good, can improve the die life several times to several times
 Manufacturing precision of the die parts of die life  
  Precision die manufacturing and life in it in particular, mold surface roughness on the mold a great impact. If using Crl2MoV steel blanking die,cnc machining parts if the surface roughness value R = 1.6 um, its life span is about 30,000. Such as polished by the precision, surface roughness value R = 0.4 m, life can be increased to 4-5 million. Therefore, the working parts of the mold surface, the general must go through grinding, grinding, polishing and other finishing and fine processing
  Other aspects of the impact of die life
  (1) Press the accuracy is not high, but also easy to make die damage.
 (2) die in the press or not installed properly and the operator's technical level, cnc machining parts on the tool life is also greatly affected.  

(3) dies in the custody and maintenance of good and bad, and the use of lubricant condition also affects mold life

 cnc machining parts

2016年5月18日星期三

Renoho Precision Machinery Technology Co.,Ltd: Die Die Life of

Renoho Precision Machinery Technology Co.,Ltd: Die Die Life of: Die Die Life of   Die Die Life of a mold material properties, chemical composition, structure, hardness and comprehensive reflection of m...

Die Die Life of

Die Die Life of 
 Die Die Life of a mold material properties, chemical composition, structure, hardness and comprehensive reflection of metallurgical quality. Among them, Precision stamping parts the material properties and heat treatment affect the quality of the most obvious.
 Mold material properties on the impact of die life is great. If the same workpiece, using a different mold material of the bending test, the test results: The 9Mn2V material, the life of 5 million; with Crl2MoV nitriding, the life of up to 40 million. Therefore, the choice of materials, the batch size should be based on workpiece, rational use of mold materials. The hardness of the die parts to Die Life a great impact. But not the higher hardness, longer die life. This is because the hardness and strength, toughness and abrasion resistance are closely related. Some die demands of high hardness, long life. Such as the use of T10 steel dies, hardness 54 ~ 58HRC, only washed thousands of times a burr on the workpiece great. Precision stamping partsIf the hardness to 60 ~ 64HRC, the grinding life of up to 2 to 3 million. However, if continue to improve hardness, fracture occurs earlier. Some die hardness should not be too high, as the die manufacturing using Crl2MoV 58 ~ 62HRC hardness, the general life of 2-3 million, invalid form of chipping and cracking, and if the hardness down to 54 ~ 58HRC, life expectancy increased to 5 ~ 60 000, but decreased to 50 ~ 53HRC hardness appears easy to blunt the die edge phenomenon.

  Thus, Precision stamping partsmold hardness must be based on material properties and failure modes may be. Should enable the hardness, strength, toughness and wear resistance, resistance to fatigue strength needed to achieve a particular stamping process the best match.

 Precision stamping parts

2016年5月15日星期日