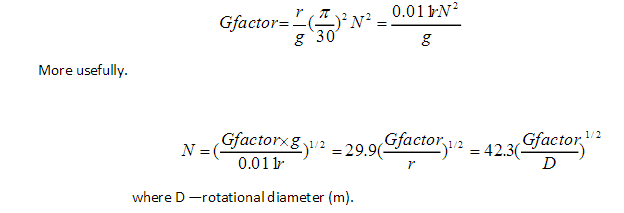2015年3月11日星期三

Introduction of Machining

Introduction of Machining 
  Speed and Feeds in Machining Speeds, feeds, China precision machining and depth of cut are the three major variables for economical machining. Other variables are the work and tool materials, coolant and geometry of the cutting tool. The rate of metal removal and power required for machining depend upon these variables. 
    The depth of cut, feed, and cutting speed are machine settings that must be established in any metal-cutting operation. They all affect the forces, the power, and the rate of metal removal. They can be defined by comparing them to the needle and record of a phonograph. China precision machining The cutting speed (V) is represented by the velocity of- the record surface relative to the needle in the tone arm at any instant. Feed is represented by the advance of the needle radially inward per revolution, or is the difference in position between two adjacent grooves. The depth of cut is the penetration of the needle into the record or the depth of the grooves. 
 Turning on Lathe Centers
   The basic operations performed on an engine lathe are illustrated. Those operations performed on external surfaces with a single point cutting tool are called turning. Except for drilling, reaming, and lapping, the operations on internal surfaces are also performed by a single point cutting tool. 
   All machining operations, including turning and boring, can be classified as roughing, finishing, or semi-finishing. The objective of a roughing operation is to remove the bulk of the material as rapidly and as efficiently as possible, while leaving a small amount of material on the work-piece for the finishing operation. Finishing operations are performed to obtain the final size, shape, and surface finish on the workpiece. Sometimes a semi-finishing operation will precede the finishing operation to leave a small predetermined and uniform amount of stock on the work-piece to be removed by the finishing operation. 
  Generally, longer workpieces are turned while supported on one or two lathe centers. Cone shaped holes, called center holes, which fit the lathe centers are drilled in the ends of the workpiece-usually along the axis of the cylindrical part. The end of the workpiece adjacent to the tailstock is always supported by a tailstock center, while the end near the headstock may be supported by a headstock center or held in a chuck. The headstock end of the workpiece may be held in a four-jaw chuck, or in a type chuck. This method holds the workpiece firmly and transfers the power to the workpiece smoothly; the additional support to the workpiece provided by the chuck lessens the tendency for chatter to occur when cutting. Precise results can be obtained with this method if care is taken to hold the workpiece accurately in the chuck.  
  Very precise results can be obtained by supporting the workpiece between two centers. A lathe dog is clamped to the workpiece; together they are driven by a driver plate mounted on the spindle nose. One end of the Workpiece is mecained;then the workpiece can be turned around in the lathe to machine the other end. The center holes in the workpiece serve as precise locating surfaces as well as bearing surfaces to carry the weight of the workpiece  and to resist the cutting forces. After the workpiece has been removed from the lathe for any reason, the center holes will accurately align the workpiece back in the lathe or in another lathe, or in a cylindricalgrinding machine. The workpiece must never be held at the headstock end by both a chuck and a lathe center. While at first thought this seems like a quick method of aligning the workpiece in the chuck, this must not be done because it is not possible to press evenly with the jaws against the workpiece while it is also supported by the center. The alignment provided by the center will not be maintained and the pressure of the jaws may damage the center hole, the lathe center, and perhaps even the lathe spindle. Compensating or floating jaw chucks used almost exclusively on high production work provide an exception to the statements made above. These chucks are really work drivers and cannot be used for the same purpose as ordinary three or four-jaw chucks.              
      While very large diameter workpieces are sometimes mounted on two centers, they are preferably held at the headstock end by faceplate jaws to obtain the smooth power transmission; moreover, large lathe dogs that are adequate to transmit the power not generally available, although they can be made as a special. Faceplate jaws are like chuck jaws except that they are mounted on a faceplate, which has less overhang from the spindle bearings than a large chuck would have. 
 Introduction of Machining 
   Machining as a shape-producing method is the most universally used and the most important of all manufacturing processes. Machining is a shape-producing process in which a power-driven device causes material to be removed in chip form. Most machining is done with equipment that supports both the work piece and cutting tool although in some cases portable equipment is used with unsupported workpiece.  
   Low setup cost for small Quantities. Machining has two applications in manufacturing. For casting, forging, and press working, each specific shape to be produced, even one part, nearly always has a high tooling cost. The shapes that may he produced by welding depend to a large degree on the shapes of raw material that are available. By making use of generally high cost equipment but without special tooling, it is possible, by machining; to start with nearly any form of raw material, so tong as the exterior dimensions are great enough, and produce any desired shape from any material. Therefore .machining is usually the preferred method for producing one or a few parts, even when the design of the part would logically lead to casting, forging or press working if a high quantity were to be produced. 
  Close accuracies, good finishes. The second application for machining is based on the high accuracies and surface finishes possible. Many of the parts machined in low quantities would be produced with lower but acceptable tolerances if produced in high quantities by some other process. On the other hand, many parts are given their general shapes by some high quantity deformation process and machined only on selected surfaces where high accuracies are needed

  Internal threads, for example,China precision machining are seldom produced by any means other than machining and small holes in press worked parts may be machined following the press working operations

 China CNC machining

2015年3月9日星期一

Basic Machining Operations and Cutting Technology

Basic Machining Operations and Cutting Technology
  Basic Machining Operations 
  China CNC machining  Machine tools have evolved from the early foot-powered lathes of the Egyptians and John Wilkinson's boring mill. They are designed to provide rigid support for both the workpiece and the cutting tool and can precisely control their relative positions and the velocity of the tool with respect to the workpiece. Basically, in metal cutting, a sharpened wedge-shaped tool removes a rather narrow strip of metal from the surface of a ductile workpiece in the form of a severely deformed chip. The chip is a waste product that is considerably shorter than the workpiece from which it came but with a corresponding increase in thickness of the uncut chip. The geometrical shape of workpiece depends on the shape of the tool and its path during the machining operation. 
  Most machining operations produce parts of differing geometry. If a rough cylindrical workpiece revolves about a central axis and the tool penetrates beneath its surface and travels parallel to the center of rotation,  China CNC machining a surface of revolution is produced, and the operation is called turning. If a hollow tube is machined on the inside in a similar manner, the operation is called boring. Producing an external conical surface uniformly varying diameter is called taper turning, if the tool point travels in a path of varying radius, a contoured surface like that of a bowling pin can be produced; or, if the piece is short enough and the support is sufficiently rigid, a contoured surface could be produced by feeding a shaped tool normal to the axis of rotation. Short tapered or cylindrical surfaces could also be contour formed.
Flat or plane surfaces are frequently required. They can be generated by radial turning or facing, in which the tool point moves normal to the axis of rotation. In other cases, it is more convenient to hold the workpiece steady and reciprocate the tool across it in a series of straight-line cuts with a crosswise feed increment before each cutting stroke. This operation is called planning and is carried out on a shaper. For larger pieces it is easier to keep the tool stationary and draw the workpiece under it as in planning. The tool is fed at each reciprocation. Contoured surfaces can be produced by using shaped tools.   
  Multiple-edged tools can also be used. Drilling uses a twin-edged fluted tool for holes with depths up to 5 to 10 times the drill diameter. Whether the   drill turns or the workpiece rotates, relative motion between the cutting edge and the workpiece is the important factor. In milling operations a rotary cutter with a number of cutting edges engages the workpiece. Which moves slowly with respect to the cutter. Plane or contoured surfaces may be produced, depending on the geometry of the cutter and the type of feed. Horizontal or vertical axes of rotation may be used, and the feed of the workpiece may be in any of the three coordinate directions. 
  Basic Machine Tools 

   Machine tools are used to produce a part of a specified geometrical shape and precise I size by removing metal from a ductile material in the form of chips. The latter are a waste product and vary from long continuous ribbons of a ductile material such as steel, which are undesirable from a disposal point of view, to easily handled well-broken chips resulting from cast iron. Machine tools perform five basic metal-removal processes: I turning, planning, drilling, milling, and grinding. All other metal-removal processes are modifications of these five basic processes. For example, boring is internal turning; reaming, tapping, and counter boring modify drilled holes and are related to drilling; bobbing and gear cutting are fundamentally milling operations; hack sawing and broaching are a form of planning and honing; lapping, super finishing. Polishing and buffing are variants of grinding or abrasive removal operations. Therefore, there are only four types of basic machine tools, which use cutting tools of specific controllable geometry: 1. lathes, 2. planers, 3. drilling machines, and 4. milling machines. The grinding process forms chips, but the geometry of the abrasive grain is uncontrollable.  
  The amount and rate of material removed by the various machining processes may be I large, as in heavy turning operations, or extremely small,  China CNC machining as in lapping or super finishing operations where only the high spots of a surface are removed.   A machine tool performs three major functions: 1. it rigidly supports the workpiece or its holder and the cutting tool; 2. it provides relative motion between the workpiece and the cutting tool; 3. it provides a range of feeds and speeds usually ranging from 4 to 32 choices in each case.

 China CNC machining

2015年3月7日星期六

Semi-centrifugal casting and Centrifuging

Semi-centrifugal casting and Centrifuging
  Semi-centrifugal casting  China CNC machining is used for jobs, which are more complicated than those possible in true centrifugal casting, but are axisymmetric in nature. It is not necessary that these should have a central hole, which is to be obtained with the help of a core. The moulds made of sand or metal are rotated about a vertical axis and the metal enters the mould through the central pouring basin as in Fig. 11.13. For larger production rates, the moulds can be stacked one over the other, China CNC machining  all feeding from the same central pouring basin. The rotating speeds used in this process are not as high as in the case of true centrifugal casting.     
  
 China CNC machining

 Centrifuging  
 In order to obtain higher metal pressures during solidification, when casting shape is not axisymmetrical, the centrifuging process is used. This is suitable only for small jobs of any shape. A number of such small jobs are joined together by means of radial runners with a central sprue on a revolving table as in Fig. 11.14. The jobs are uniformly placed on the table around the periphery so that their masses are properly balanced. China CNC machining  The process is similar to semi-centrifugal casting.

   
 China precision machining

2015年3月5日星期四

Renoho Precision Machinery Technology Co.,Ltd: True centrifugal casting

Renoho Precision Machinery Technology Co.,Ltd: True centrifugal casting: True centrifugal casting     This is normally  China CNC machining   used for the making of hollow pipes, tubes, hollow bushes, etc., whi...

True centrifugal casting

True centrifugal casting  
 This is normally China CNC machining used for the making of hollow pipes, tubes, hollow bushes, etc., which are axisymmetric with a concentric hole. Since the metal is always pushed outward because of the centrifugal force, no core needs to be used for making the concentric hole. The axis of rotation can be either horizontal, vertical or any angle in between. Very long pipes are normally cast with horizontal axis, whereas short pieces are more conveniently cast with a vertical axis.   
    
 China precision machining

                              
 A normal centrifugal casting machine used for making cast iron pipes in sand mould is shown in Fig. 11.12. First, the moulding flask is properly rammed with sand to confirm to the outer contour of the pipe to be made. Any end details, such as spigot ends, or flanged ends are obtained with the help of dry sand cores located in the ends. Then the flask is dynamically balanced so as to reduce the occurrence of undesirable vibrations during the casting process. The finished flask in mounted in between the rollers and the mould is rotated slowly. Now the molten metal poured determines the thickness of the pipe to be cast. China CNC machiningAfter the pouring is complete, the mould is rotated at its operational speed till it solidifies, to form the requisite bubing. Then the mould is replaced by a new mould machine and the process continued.    
   Metal mould can also be used in the true centrifugal casting process for large quantity production. A water jacket is provided around the mould for cooling it. The casting machine is mounted on wheels with the pouring ladle, which has a long spout extending till the other end of the pipe to be made. To start, the mould is rotated with the metal being delivered at the extreme end of the pipe. The casting machine is slowly moved down the track allowing the metal to be deposited all along the length of the pipe. 
  The machine is China CNC machining continuously rotated till the pipe is completely solidified. Afterwards, the pipe is extracted from the mould and the cycle repeated.      

2015年3月3日星期二

Centrifugal Casting


Centrifugal Casting
   China metal parts machining Centrifugal casting consists of having sand, metal, or ceramic mold that is rotated at high speeds. When the molten metal is poured into the mold it is thrown against the mold wall, where it remains until it cools and solidifies. The process is being increasingly used for such products as cast-iron pipes, cylinder liners, gun barrels, pressure vessels, brake drums gears, and flywheels. The metals used include almost all castable alloys. Because of the relatively fast cooling time, centrifugal castings have a fine gram size. There is a tendency for the lighter non-metallic inclusions slagparticles, and dross to segregate toward the inner radius of the casting where it can be easily removed by machining. Due to the high purity of the outer skin, centrifugally cast pipes have a high resistance to atmospheric corrosion. 
  The principle of centrifugal casting is shown as Fig. 11.11. The centrifugal force produced by rotation is large compared with normal hydrostatic forces and is utilized in two ways. The first of these is seen in pouring, where the force can be used to distribute liquid metal over the outer surfaces of a mould. This provides a means of forming hollow cylinders and other annular shapes. The second is the development of high pressure in the casting during freezing. This, in conjunction with directional solidification, assists feeding and accelerates the separation of non-metallic inclusions and precipitated gases. The advantages of the process are therefore twofold: suitability for casting cylindrical forms and high metallurgical quality of the product. 
   The casting  China metal parts machining of a plain pipe or tube is accomplished by rotation of a mould about its own axis, the bore shape being produced by centrifugal force alone and the wall thickness determined by the volume of metal introduced. This practice is widely referred to as true centrifugal casting. In
the case of a component of varying internal diameter or irregular wall thickness a central core may be used to form the internal contours, feeder heads then being introduced to compensate for solidification shrinkage. A further step away from the original concept is the spacing of separate shaped castings about a central down-runner, which forms the axis of rotation. These variations are referred to respectively as semicentrifugal casting and centrifuging or pressure casting; in both cases, since the castings are shaped wholly by the mould and cores, centrifugal force is used primarily as a source of pressure for feeding.

 China CNC machining

The rotational axis may be horizontal, vertical or inclined and important variations exist in respect of mould material and the method of introduction of the molten metal.
    The centrifugal force acting upon a rotating body is proportional to the radius of rotation and to the square of the velocity:               
 China CNC machining

    
The gravitational force on the same mass would be given by:

 China CNC machining

Hence the factor by which the normal force of gravity is multiplied during rotation is given by:
 China CNC machining

Expressed in the more convenient speed units of revolutions per minute, N, the expression becomes:
 china machining manufacturer

  Although centrifugal forces exceeding 200G are attained in some cases, most practice is empirically based within the range 10-150G, the highest values being used for open bore cylindrical components of small diameter and the lowest for semicentrifugal and pressure castings. Speeds generating forces of 60-80G are most commonly quoted for true centrifugal castings. As previously emphasized, however, the optimum value of centrifugal force diminishes with increasing diameter.    
    Cumberland quotes values of 33G for a wide range of plain vertical axis castings and 15G for semi-centrifugal castings in sand moulds, for which lower speeds suffice since there is no longer dependence on centrifugal force to shape the casting. Thornton gives values of 50-100G for die cast and 25-50G for sand castpots and shaped castings.     

    This is a process where the mould is rotated rapidly about its central axis as the metal is poured into it. Because of the centrifugal force, a continuous pressure will be acting on the metal as it solidifies. The slag, oxides and other inclusions being lighter, get separated from the metal and segregates toward the centre.  China metal parts machining There are three main types of centrifugal casting processes. They are: true centrifugal casting, semi-centrifugal casting, centrifuging.      

2015年3月1日星期日

Vacuum Casting and Continuous Casting

Vacuum Casting and Continuous Casting
 Vacuum Casting
 Vacuum casting is similar China CNC machining to Low Pressure Die Casting in that a permanent mould is linkedto a crucible of molten metal by a riser tube, but instead of pressure being applied to themolten metal, a vacuum is created in the mould cavity, thus drawing the metal up into the cavity.
 Continuous Casting
  Generally the starting point of any structural steel product is the ingot which is subsequently rolled through number of mills before a final product. However, the wide adoption of continuous casting has changed that scenario by directly casting slabs,billets and blooms without going through the rolling process. This process is fast and also economical.
   Continuous casting is the process whereby molten steel is solidified into a semifinished billets, blooms, China CNC machining or slabs for subsequent rolling in finishing mills.
In continuous casting, liquid steel is transferred in a ladle to the casting machine. When the casting operation starts, the sliding shutter at the bottom of the ladle is opened and the steel flows at a controlled rate into the tundish and from the tundish into one or more molds The liquid steel is poured into a double walled, bottomless water cooled mould where a solid skin is quickly formed and a semi-finished skin energy form the open mould bottom. The skin formed in the mould is about 10 to 25 mm in thickness and is further solidified by intensive cooling with water spays as casting moves downwards. About 55 percent of the world's liquid steel production is solidified in continuous casting processes, the most widely used of which feeds liquid steel continuously into a short, water-cooled vertical copper mold and, at the same time, continuously withdraws the frozen shell, including the liquid steel it contains. 
                Fig. 11.9 Schematic of continuous casting process   

 China precision machining

 A typical arrangement of continuous casting plant is shown schematically in Fig. 11.9. The molten steel is collected in a ladle and kept over a refractory lined intermediate pouring vessel named tundish. The steel is taken poured into water cooled vertical cooper moulds which are 450 to 750 mm long. Before starting the casting a dummy starter bar is kept in the moulds bottom as shown in Fig.11.9. After starting the casting process as the metal level rises in the mould to a desirable height, the starter bar is withdrawn at a rate equal to the steel pouring rate. The initial metal freezes onto the starter bar as well as the periphery of the mould. This solidified shell supports the liquid steel as it moves downwards. This steel shell is mechanically supported (rollers) as it moves down through the secondary cooling zone where water is spried onto the shell surface to complete the solidification process. After the casting is completely solidified, it is cut to the desired lengths by a suitable cutoff apparatus.
  To appreciate fully the substantial benefits of continuous casting it is necessary to review some aspects of modern steelmaking and the older process of ingot casting. 
 In both processes, molten steel (usually called a “heat”) is prepared or an electric furnace. The in an oxygen furnace, an open-hearth furnace molten steel is next transferred in a ladle to either a nearby ingot or continuous casting facility. 

 Various types of ingots are prepared, in both processes, depending on the size and shape of the final steel products to be manufactured. China CNC machiningThree types of ingots are made: billets, blooms and slabs. Slabs are used to make plate and other flat products. Billets and blooms are used to make structural shapes, round products and tubes.